Control devices on an aging production line are still generating data, but nobody is looking at it.
In the workshop of a food packaging plant, three Mitsubishi PLCs manage the entire packaging line. Temperature, humidity, runtime, and downtime counts are stored inside the local controllers. Operators walk the floor before shift end, record readings on paper, and file them away. By the time those numbers make it onto a report, production has already stopped. Preventive maintenance or downtime optimization based on that data is not realistic.
This pattern shows up frequently in solutions designed by equipment manufacturers. Customers rarely have a brand-new automation line. They have equipment that has been running for years. The machines work, the data keeps coming, but there is no channel to send it anywhere useful.
The core approach is straightforward: add an industrial gateway as a bridge.
The gateway sits beside the legacy equipment, reads PLC data through serial or Ethernet ports, and pushes that data to the cloud. The PLC itself stays untouched—no model swap, no reprogramming. The production line keeps running, and a new data path to the cloud is simply added on top.
PLCs were born from industrial control needs, where the design goals were stability, real-time response, and repeatability. PLCs deployed from the 1990s through the early 2000s generally offered only serial communication, with Modbus RTU as the dominant protocol. Some models from the mid-2000s added an Ethernet port, but the protocol stack revolved around Modbus TCP and Profibus, with no built-in MQTT, HTTP, or other internet-facing connection methods.
In other words, these PLCs can talk to local HMIs and SCADA systems, but cannot connect directly to cloud platforms. Data stays trapped inside the device, visible only to someone standing right next to it.
This is not a flaw with the PLC. It was a deliberate design choice shaped by the context of the time. Industrial networks at that stage were designed to exchange data within the workshop floor. Internet connectivity was simply not on the requirement list.
The industrial gateway plays two roles: protocol translator and data relay.
Step one: read PLC data.An industrial IoT gateway such as the USR-M300 is equipped with RS485 and Ethernet ports. The RS485 port connects directly to the PLC serial port, reading register values via Modbus RTU. The Ethernet port handles newer control devices that speak Modbus TCP. A single gateway processes both serial and network data simultaneously, eliminating the need for different devices per protocol.
The USR-M300 supports parallel acquisition, pulling data from multiple serial ports, Ethernet ports, and IO devices at once, handling up to 2,000 data points.
Step two: protocol conversion.The data coming out of the PLC is a raw Modbus register value—a temperature register reads 256, which corresponds to 25.6℃. The gateway performs unit conversion and data formatting locally, turning raw register values into structured JSON. This happens at the gateway edge, so the cloud platform receives clean data without requiring additional processing.
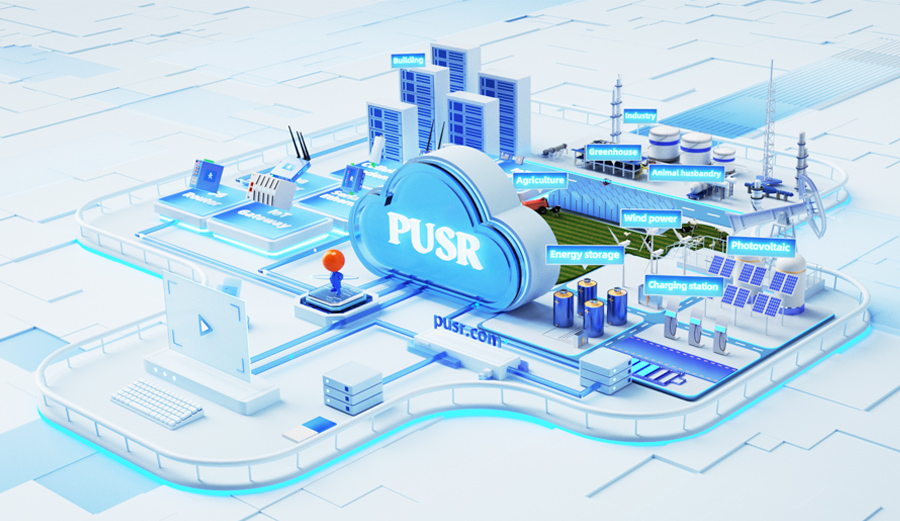
Step three: cloud delivery.The USR-M300 has a built-in MQTT stack and pushes data to the cloud via 4G or Ethernet. It supports Alibaba Cloud, AWS, Azure, ThingsBoard, and PUSR Cloud, along with standard MQTT and TCP protocols for custom or self-hosted platforms. One path handles the upload.
If no wired network exists at the site, the USR-M300 also supports LTE 4G and 3G wireless connectivity with an external antenna, eliminating the need for cabling.
Not all data needs to go to the cloud.
Consider an injection molding machine where an overtemperature threshold triggers an alarm. The alarm message needs to reach the workshop operator immediately—not the cloud database. High-real-time logic sent to the cloud introduces network latency and unnecessary round trips.
The USR-M300 includes Node-RED, a graphical programming environment that lets users build data-flow logic directly on the gateway. Nodes are dragged, parameters are set, and data processing, conditional checks, and message routing are complete. An overtemperature alarm triggers locally on the gateway, while only statistical and reporting data gets sent to the cloud. This reduces both cloud data volume and network dependency.
Interface matching.Check the PLC communication interface—RS232, RS485, or Ethernet—and choose the corresponding gateway port. The USR-M300 provides one RS232/485 and one RS485 port, covering the serial communication needs of most PLCs.
Data point count.Estimate the register address range that needs to be collected, and confirm the gateway's data point capacity is sufficient. The USR-M300 supports up to 2,000 data points in parallel acquisition, which is adequate for small to medium production lines.
Power supply environment.Older installations often have less-than-ideal power conditions. The USR-M300 accepts DC 9~36V wide-voltage input and operates reliably between -25℃ and 75℃, meeting the harsh environment demands of factory workshops.
Installation method.The unit supports DIN-rail and wall mounting, selected based on the available space inside the control cabinet.
Adding cloud connectivity to legacy equipment without replacing the PLC is best achieved through an industrial gateway. Protocol translation, edge computing, and wireless upload are all integrated into a single device, wired directly beside the existing equipment and ready to go.
Data does not need to stay locked inside a decades-old controller. Add a gateway, and the production line's data can flow to the cloud.